Why Anthracite Coal Is Ideal for Activated Carbon Production
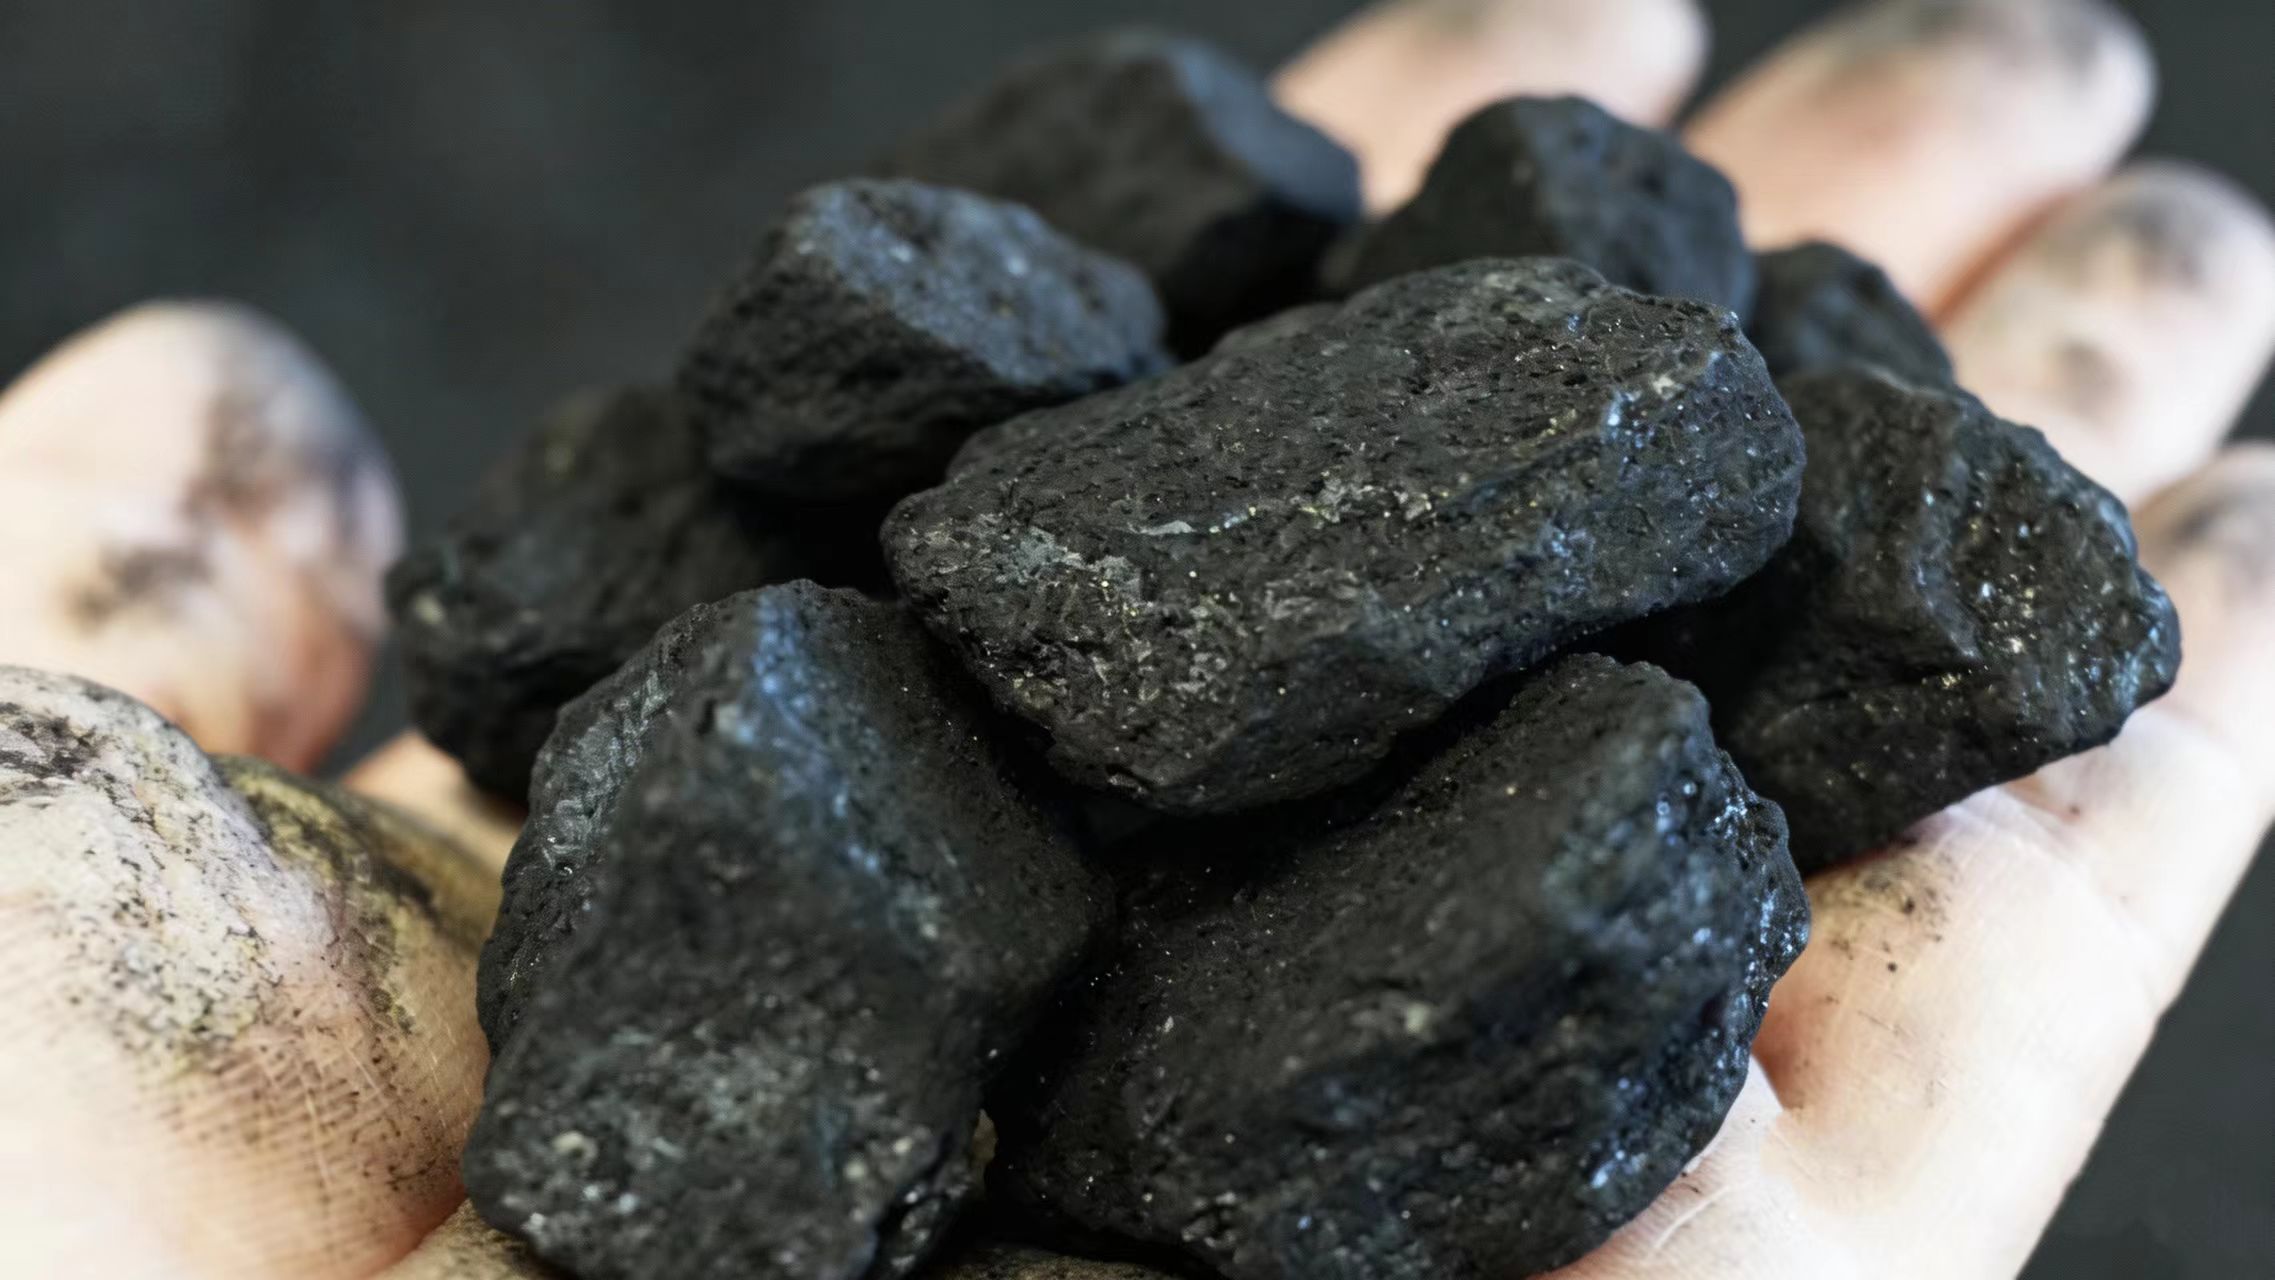
The quality of activated carbon largely depends on the raw material used during production. Among all carbon sources, anthracite coal is widely recognized as one of the best materials for manufacturing high-performance activated carbon.
Due to its high carbon content, low impurities, and excellent physical strength, anthracite coal plays a key role in producing activated carbon for water treatment, air purification, and industrial applications.
What Is Anthracite Coal?
Anthracite coal is the highest rank of coal, formed over millions of years under high pressure and temperature. It contains the highest fixed carbon content and the lowest volatile matter compared to other types of coal.
Because of its dense structure and low impurity levels, anthracite is highly suitable for producing high-quality activated carbon.
Key Properties That Make Anthracite Ideal for Activated Carbon
- High Carbon Content: Provides strong adsorption foundation
- Low Ash Content: Ensures higher purity activated carbon
- High Hardness: Improves mechanical strength and reduces breakage
- Stable Structure: Ensures consistent production quality
- Low Volatile Matter: Improves carbonization efficiency
How Anthracite Coal Is Used in Activated Carbon Production
The production process of coal-based activated carbon typically includes crushing, carbonization, and activation. Anthracite coal serves as the primary raw material in this process.
First, the coal is carbonized at high temperature to remove volatile components. Then it undergoes activation using steam or chemical agents to develop a porous internal structure.
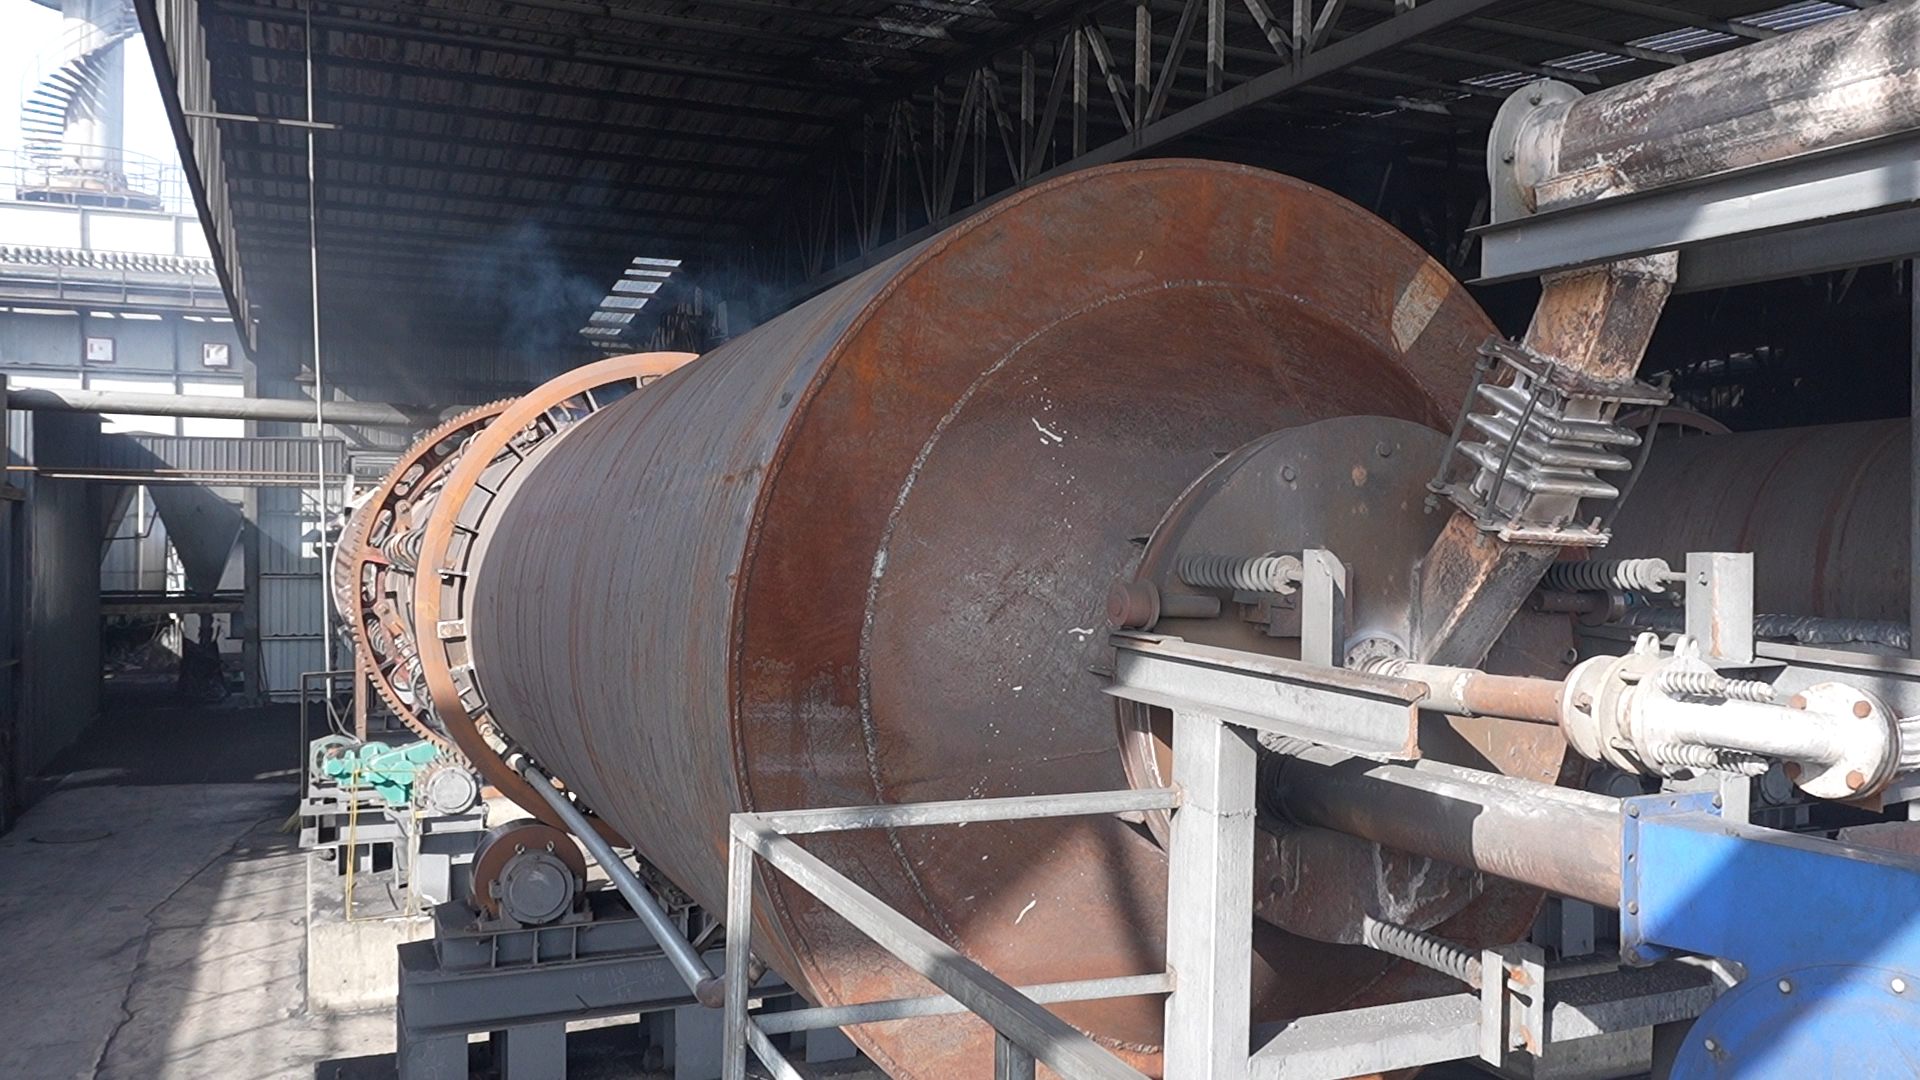
Learn more about our production process here: Activated Carbon Production Process
Applications of Anthracite-Based Activated Carbon
Activated carbon produced from anthracite coal is widely used in many industries:
- Water Treatment Systems
- Wastewater Treatment Plants
- Air Purification Systems
- Food and Beverage Industry
- Chemical Processing Industry
- Gold Recovery
Explore more applications: Activated Carbon Applications
Why Choose Our Anthracite-Based Activated Carbon?
As a professional activated carbon manufacturer, we use high-quality anthracite coal as raw material and operate advanced production lines to ensure stable product performance.
- High adsorption capacity
- Custom particle size available
- Stable supply capability
- Strict quality control system
- Competitive factory pricing
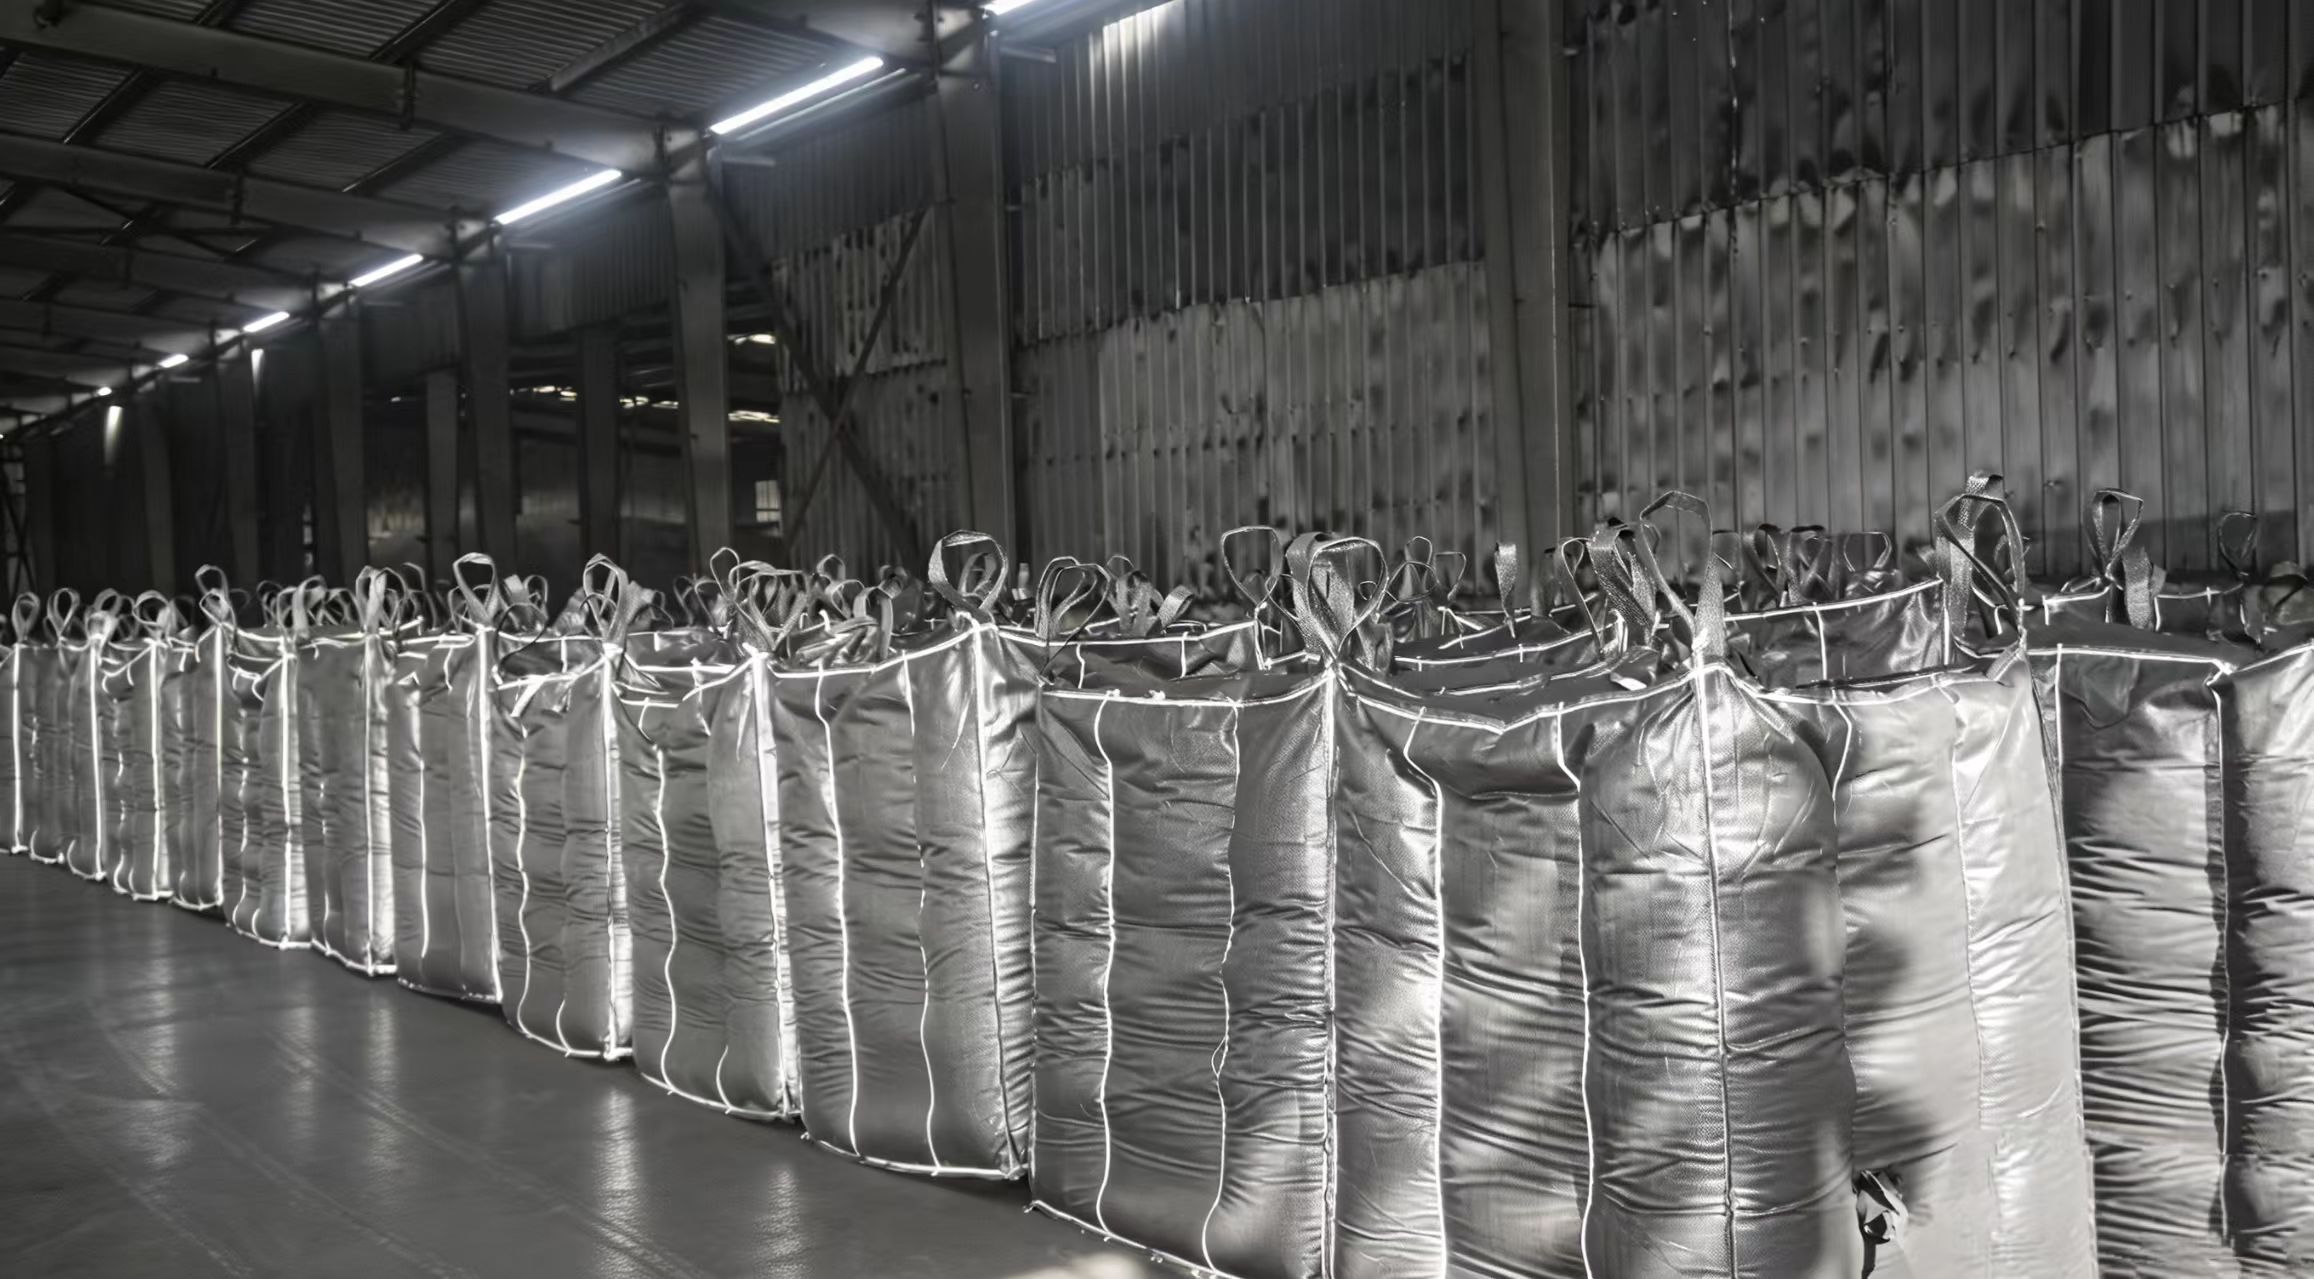
View our product range: Activated Carbon Products
Conclusion
Anthracite coal is one of the most suitable raw materials for activated carbon production due to its high carbon content, low impurities, and strong physical properties.
Its use ensures high-quality activated carbon with excellent adsorption performance, making it ideal for industrial water treatment and environmental applications.
Looking for High-Quality Activated Carbon?
Contact us for product specifications, pricing, and samples.
Get a Quote Now →We will reply within 24 hours.